Die Casting Startup Costs: A Guide to Molds & Manufacturing | EasoonMade
Sep 17,2026 | Tommy
Die casting startup costs?
A common moment of "sticker shock" for first-time hardware founders: an inventor with a patent-pending design — say, a 10-inch, hollow, thin-walled part — moves from a validated CAD file toward actual production and asks the plain question: how much will a manufacturer actually charge, and what does setting up the molds cost?
The gap between a $50 3D-printed prototype and a real production line can feel like stepping into a different financial category entirely. This guide breaks down what die casting startup costs actually look like for a hollow part like this, why the "hollow" detail matters more than it seems, and how to avoid overpaying on a first production run.
TL;DR: The Executive Summary
For a 10-inch hollow aluminum part, die casting tooling typically runs $20,000–$55,000, with a very low per-unit cost afterward (often $5–$15). One critical technical constraint: steel cannot be high-pressure die cast, so a steel version of this part requires Investment Casting instead — lower tooling cost ($4,000–$10,000) but a higher per-unit price. For a startup still validating market interest, Gravity Casting or rapid soft tooling is the more sensible starting point before committing to a $40,000+ high-pressure mold.
The Pain Points: Why "Startup" and "Die Casting" Often Clash
Tooling Sticker Shock. Many first-time founders expect mold costs in the low thousands. A $35,000 quote can stop a project before it starts, simply from the size of the number relative to early-stage budgets.
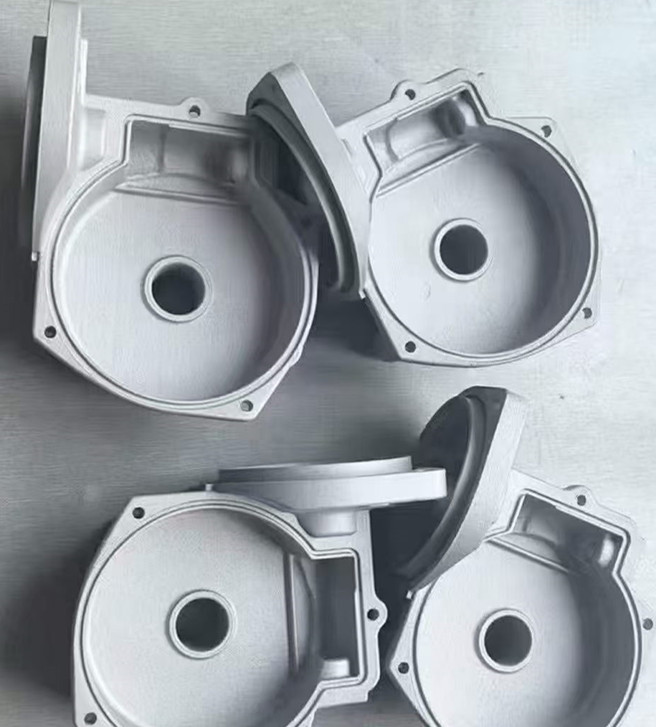
The Complexity of "Hollow." A hollow 10-inch part requires cores or slides inside the mold — moving mechanical components that meaningfully increase both the mold's complexity and its price compared to a solid part of the same size.
Material Confusion. "Aluminum or steel" often gets treated as interchangeable in early planning, but these require entirely different processes, temperatures, and tooling approaches in casting — the choice isn't a late-stage detail, it's foundational.
Volume Requirements. Most die casting houses won't run their machines for orders under 2,000–5,000 units, which creates a real cash-flow wall for a startup that only wants to validate demand with 500 pieces.
Design Rigidity Once Committed. After $30,000 goes into a hardened steel mold, the design is effectively frozen — if early customer feedback suggests a change, that investment can't easily absorb it.
5 Solutions to Manage Die Casting Startup Costs
- Validate the Design With CNC or Metal 3D Printing First Before any mold conversation, the first 1–10 units should come from CNC machining a solid block or metal 3D printing. Per-unit cost is high ($500+), but startup cost is effectively zero — and this stage is what confirms thin walls hold up structurally and the hollow interior doesn't create unexpected cooling or stress issues once the design moves to actual casting.
- Gravity (Permanent Mold) Casting for the 100–1,000 Unit Range When the goal is validating market interest at moderate volume, high-pressure die casting tooling is overkill. Gravity casting uses iron or steel molds without the hydraulic pressure system, and tooling for a part this size might run $5,000–$12,000 — roughly 70% lower entry cost than high-pressure tooling, with a slightly rougher surface finish as the trade-off.
- Investment Casting as the Steel Solution Steel's melting point is too high for a traditional die-casting mold — the mold itself would fail alongside the part. Investment (lost-wax) casting sidesteps this: tooling is a simple aluminum mold used to produce wax patterns, keeping startup cost in the $3,000–$8,000 range, though the more labor-intensive process pushes per-part cost higher. For a 10-inch hollow steel part at startup scale, this is realistically the only viable path.
- High-Pressure Die Casting Once Volume Justifies It Past roughly 5,000 units, high-pressure die casting becomes the most efficient process available. For a part this size, a 400–800 ton cold-chamber machine is typically required, with total startup tooling — mold base, cavity/core machining, and the slides needed for the hollow center — landing around $35,000 or more. Family molds or modular inserts can help amortize this cost across multiple related parts.
- DFM to Reduce What the Mold Actually Has to Do A manufacturer's quote reflects difficulty, not just size. Splitting the 10-inch part into two halves that bolt or weld together can eliminate the need for expensive internal cores. Increasing draft angle lets the part eject faster, reducing machine cycle time and lowering per-part cost — both changes that come from the design side, not the manufacturing side.
Comparison: Startup Costs by Process (10-Inch Hollow Part)
|
Feature |
CNC Machining |
Investment Casting |
Gravity Casting |
High-Pressure Die Casting |
|
Material |
Aluminum / Steel |
Steel / Aluminum |
Aluminum |
Aluminum / Magnesium |
|
Tooling Cost |
$0 |
$3k–$8k |
$6k–$12k |
$25k–$55k |
|
Unit Price |
$400–$800 |
$40–$70 |
$25–$45 |
$8–$15 |
|
Lead Time |
1 Week |
5–7 Weeks |
6–8 Weeks |
10–12 Weeks |
|
Best Volume |
1–20 pcs |
50–500 pcs |
200–2,000 pcs |
5,000+ pcs |
FAQ: Navigating the Startup Journey
Q: Why does the mold cost so much relative to the part itself? A: A die-casting mold is a precision machine in its own right — typically H13 hardened tool steel engineered to withstand thousands of pounds of pressure and repeated extreme heat cycles. The quote covers engineering, cavity machining, heat treatment, and the initial test shots (T1 samples) that validate the tool before production begins.
Q: Do I actually own the mold once it's paid for? A: That depends entirely on the agreement — with a straightforward arrangement, tooling belongs to the client once paid, even if the manufacturer stores and maintains it. It's worth watching for unusually low tooling quotes where the manufacturer quietly retains ownership.
Q: How thin can the walls of a hollow part actually be without cracking? A: This is where mold flow analysis matters — simulating how the liquid metal fills the mold to check whether thin sections cool too quickly. If a wall is genuinely too thin for a 10-inch span, adding internal ribs for structural support is a common fix.
Q: Can the same mold be used for both aluminum and zinc? A: Generally no — the two metals have different shrinkage rates and melting temperatures, so a mold designed around aluminum's behavior will produce out-of-spec zinc parts.
Q: What's the realistic first step for a patent-holder with a limited budget? A: Prove the design with CNC prototypes first, validate market interest with rapid/soft tooling in the sub-$10,000 range, and only move to full high-pressure die casting once order volume genuinely justifies that investment.
Why the Right Manufacturing Partner Matters for This Journey
The frustration in "how much will a manufacturer demand for this" usually comes from not understanding what's actually being paid for. As a patent-holder, budget is finite and the risk of getting it wrong is real — which is why a transparent roadmap matters more than a single number: CNC prototypes to prove the design, rapid tooling to enter the market under $10,000, and precision multi-cavity die casting molds once volume justifies the "big league" investment.
Ready to see what your 10-inch part will actually cost? Upload your CAD file today for a transparent, comprehensive casting quote from EasoonMade.
Comment