Custom Aluminum Intake Manifold Manufacturing | EasoonMade
Sep 12,2026 | Tommy
Why Does a "Bolt-On" Custom Intake Manifold Never Actually Bolt On?
Search any turbo-swap or engine-building forum long enough and you'll find a version of this frustration: someone orders a custom or aftermarket intake manifold advertised as a direct bolt-on, and it arrives needing port matching, injector boss rework, or outright doesn't clear the firewall or intercooler piping on their specific engine bay. The seller calls it "universal fit." The builder calls it a weekend lost to a die grinder.
This gap between an off-the-shelf manifold and a part that actually performs on a specific engine and chassis combination is one of the most common frustrations in performance engine building — and it's almost entirely solvable with the right manufacturing approach.
This guide breaks down why generic intake manifolds fail to fit and flow as promised, and the manufacturing methods that actually deliver a manifold built for your engine, your turbo, and your engine bay.
TL;DR: The Executive Summary
Off-the-shelf intake manifolds are designed around a generic engine block and injector spacing, which is why "universal" fitment so often means grinding, shimming, or re-drilling. The reliable fix is a manufacturing process built around your actual hardware: 3D scanning of the block and head to capture true mounting geometry, CNC-machined billet aluminum or A356 cast-and-machined construction for the plenum and runners, and CFD-informed runner geometry to balance cylinder-to-cylinder airflow rather than just maximizing peak flow. EasoonMade delivers this as a single reverse-engineering-to-finished-part workflow, so the manifold that arrives is the manifold that bolts on.
The Pain Points: Why Custom Intake Manifolds Are Hard to Get Right
Generic Fitment Data. Most aftermarket manifolds are designed from a single "representative" block sample, not your specific engine, head casting revision, or injector configuration — so bolt patterns, injector bosses, and throttle-body flanges that look correct on the spec sheet don't always align in the car.
Runner Length and Plenum Volume Trade-offs. Longer runners build low-end torque; shorter runners favor top-end power. A plenum sized wrong for the turbo or throttle body creates flow imbalance between cylinders — an issue that doesn't show up until the engine is under load on a dyno.
Casting Porosity Under Boost. For cast manifolds, internal porosity that would be a non-issue on a naturally aspirated engine becomes a boost-leak or crack risk once positive manifold pressure is introduced.
Clearance Conflicts in the Engine Bay. A manifold that flows perfectly on a flow bench can still be unusable if it doesn't clear the firewall, intercooler piping, brake booster, or other accessories specific to the chassis it's going into.
Injector Angle and Fuel Delivery Mismatch. Injector bosses machined at a generic angle can create poor fuel atomization or spray-pattern interference with the runner wall, hurting both efficiency and cylinder-to-cylinder consistency.
5 Specific Solutions for Custom Intake Manifolds That Actually Fit and Flow
- 3D Scanning the Actual Engine and Chassis, Not a Generic Reference We scan your specific cylinder head mounting face, injector bosses, and — where clearance is tight — the surrounding engine bay geometry, so the manifold's mounting flange and physical envelope are built from your hardware, not an averaged reference block.
- CFD-Informed Runner and Plenum Design Before any metal is cut, runner length, cross-section, and plenum volume are modeled to balance airflow across all cylinders for your specific turbo, displacement, and target power band — rather than defaulting to the largest possible plenum and hoping for the best.
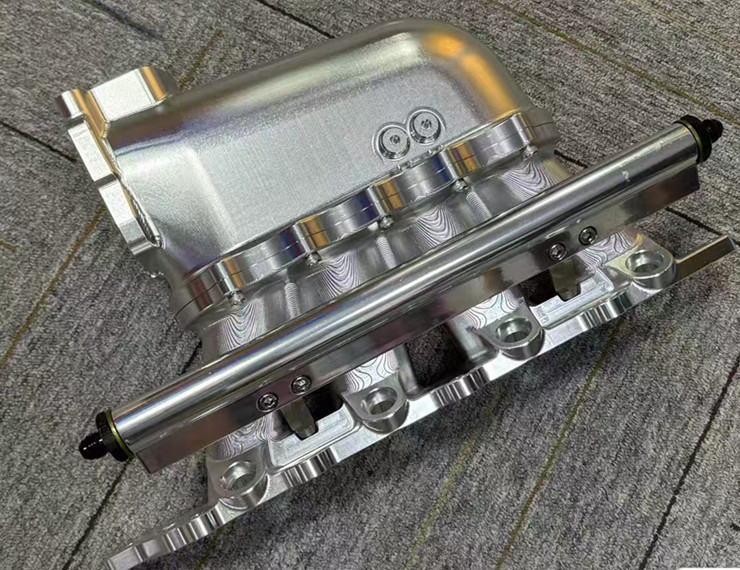
- CNC Billet Machining for High-Boost Applications For turbo and high-boost naturally-aspirated builds, we machine the manifold from solid 6061-T6 billet aluminum. This eliminates porosity entirely and allows internal runner geometry that would be difficult or impossible to cast cleanly.
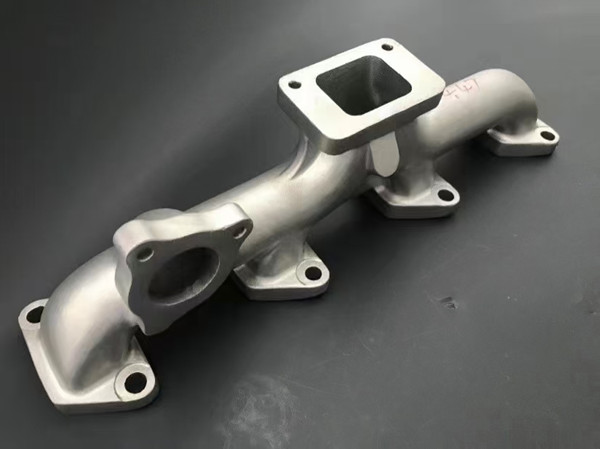
- A356 Cast-and-Machined Construction for Cost-Sensitive Runs For naturally aspirated or moderate-boost applications where billet cost isn't justified, we cast in A356 aluminum with rotary degassing to control porosity, then CNC-machine the mounting flange, injector bosses, and throttle-body face for precise fitment.
- Injector Boss Angle Matched to Your Fuel System Injector bung angle and depth are set to match your specific injector length and spray pattern, verified against the runner CAD model before machining — avoiding the atomization and clearance issues that come from a one-angle-fits-all boss design.
Comparison: Which Manifold Construction Fits Your Build?
|
Feature |
Stock/Cast OEM |
Sheet Metal Fabricated |
A356 Cast + Machined |
CNC Billet Aluminum |
|
Best For |
Stock power levels |
One-off race builds |
Moderate boost, cost-conscious builds |
High boost, max airflow customization |
|
Runner Geometry Freedom |
None |
High |
Moderate |
Very High |
|
Porosity Risk |
Low (OEM QC) |
None (welded, not cast) |
Low (with degassing) |
None |
|
Fitment Precision |
Exact (OEM only) |
Depends on fabricator |
High (with 3D scan input) |
Highest |
|
Typical Lead Time |
N/A |
2–4 Weeks |
3–5 Weeks |
2–3 Weeks |
FAQ: Common Questions About Custom Intake Manifold Manufacturing
Q: Can you build a manifold from just my old, damaged one? A: In most cases, yes. We 3D scan the existing part (or the remaining pieces if it's cracked), reconstruct clean CAD geometry, and can incorporate design improvements like larger runners or a repositioned throttle-body flange along the way.
Q: Is billet or cast better for a turbo application? A: For anything running significant boost, billet eliminates porosity risk entirely and gives more freedom for complex runner shapes. Cast-and-machined is a cost-effective option for moderate boost when porosity is controlled through proper degassing.
Q: How do you avoid the clearance problems generic manifolds have? A: By scanning the actual engine bay constraints relevant to your build — firewall position, intercooler piping routing, brake booster location — before finalizing the manifold's physical envelope, not after.
Q: Will you dyno-tune the manifold design for my specific turbo? A: We model runner and plenum sizing using CFD analysis against your stated turbo, target boost, and power goals to balance cylinder airflow before manufacturing. Final tuning on your dyno is still recommended once the manifold is installed.
Q: What's a typical cost range for a custom intake manifold? A: Cost depends heavily on construction method and complexity — cast-and-machined manifolds are typically the more economical route, while fully CNC-billet manifolds cost more upfront but eliminate porosity risk and allow the most aggressive runner designs. Contact us for a quote specific to your engine and goals.
Why Choose EasoonMade for Your Custom Intake Manifold?
The "universal fit" problem in aftermarket intake manifolds comes down to one thing: the part was designed around a generic reference, not your actual engine and chassis. At EasoonMade, every custom manifold starts with your real hardware — scanned, modeled, and airflow-balanced before a single part is machined or cast — so what arrives is built to bolt on and perform, not to be modified into submission.
Ready to build a manifold that fits the first time? Submit your engine and turbo specs to EasoonMade for a professional engineering review and quote today.
Comment